Manufacturer and Exporter of Sintered Bronze Filter Elements
The best Manufacturer of Sintered Bronze Silencer in Pune, India
In India’s heavy industries, reliability and cost efficiency are non-negotiable. From cement kilns to chemical reactors, the demand for robust, long-lasting filtration solutions is higher than ever. At the center of this industrial revolution are industrial sintered filters — a technology that balances durability, reusability, and precision.
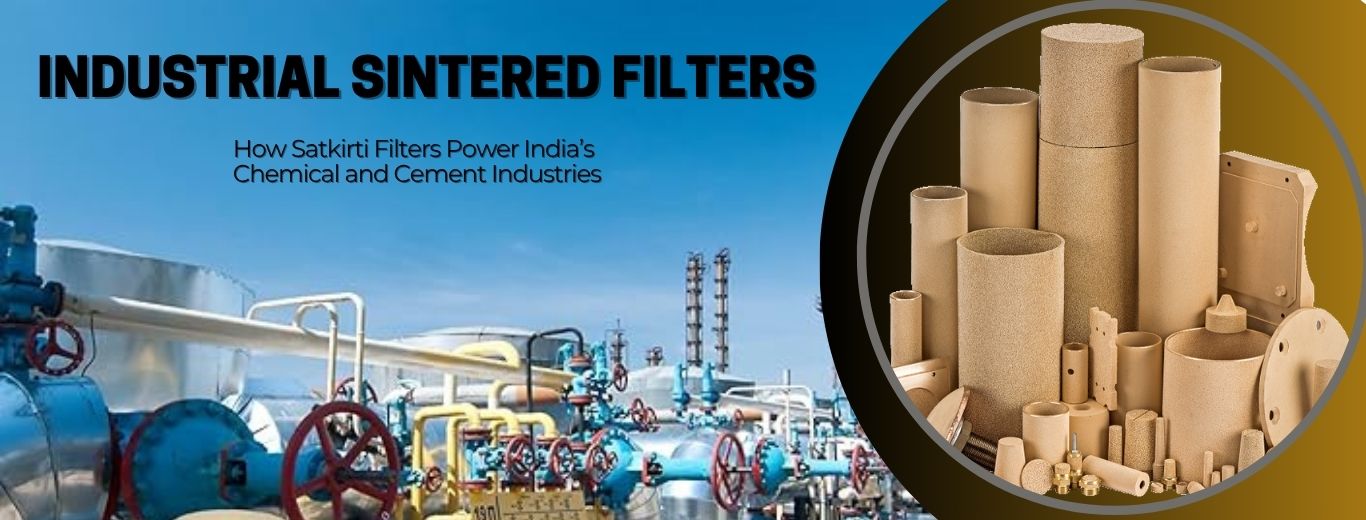
For over a decade, Satkirti Filters has been at the forefront of supplying customized industrial sintered filters to leading cement and chemical plants across India. In this spotlight, we’ll explore how these filters deliver measurable value in two of the most challenging verticals: cement production and chemical processing.
Unlike disposable filter media, industrial sintered filters are engineered using powdered metals such as bronze and stainless steel, sintered at high temperatures to create a rigid, porous structure. The result is:
These characteristics make them indispensable in industries where filtration quality directly impacts productivity, safety, and costs.
Cement plants face one of the harshest operating conditions—high dust loads, elevated temperatures, and abrasive particles. Traditional filters clog quickly, leading to:
One leading cement manufacturer in Central India was replacing disposable filters every 3 weeks, creating downtime losses of ₹8–10 lakhs annually.
Satkirti engineered a line of industrial sintered filters specifically designed for cement kiln exhaust systems. Features included:
By switching to Satkirti’s industrial sintered filters, the cement plant not only cut costs but also achieved stable process efficiency and compliance with emission norms.
Chemical plants deal with aggressive fluids, corrosive vapors, and volatile environments. Disposable filters degrade quickly under such conditions, leading to:
A specialty chemical producer in Gujarat faced recurring clogging issues in their solvent recovery lines, forcing filter replacements every 10 days.
Satkirti supplied stainless steel industrial sintered filters with corrosion-resistant properties, engineered for fine micron ratings and solvent compatibility. The filters were also designed for ultrasonic cleaning, allowing technicians to restore them instead of replacing them.
The adoption of Satkirti’s industrial sintered filters transformed the plant’s reliability while cutting lifecycle costs dramatically.
Depending on application, filters last 6 months to several years with proper cleaning cycles.
Yes. Satkirti offers stainless steel and alloy sintered filters specifically for chemical resistance.
Plants often achieve 30–50% cost savings annually, plus reduced downtime and waste.
In industries as demanding as cement and chemicals, reliability is not optional—it’s the backbone of productivity. Satkirti Filters has proven that industrial sintered filters are more than just a product; they’re a long-term investment in efficiency, safety, and cost savings.
By partnering with Satkirti, India’s leading plants are reducing downtime, extending equipment life, and meeting sustainability goals—all while lowering total ownership costs.
CTA: Looking to upgrade your plant’s filtration systems? Contact Satkirti Filters today to discover custom-engineered sintered solutions for your industry.